Cylinder Liner Honing
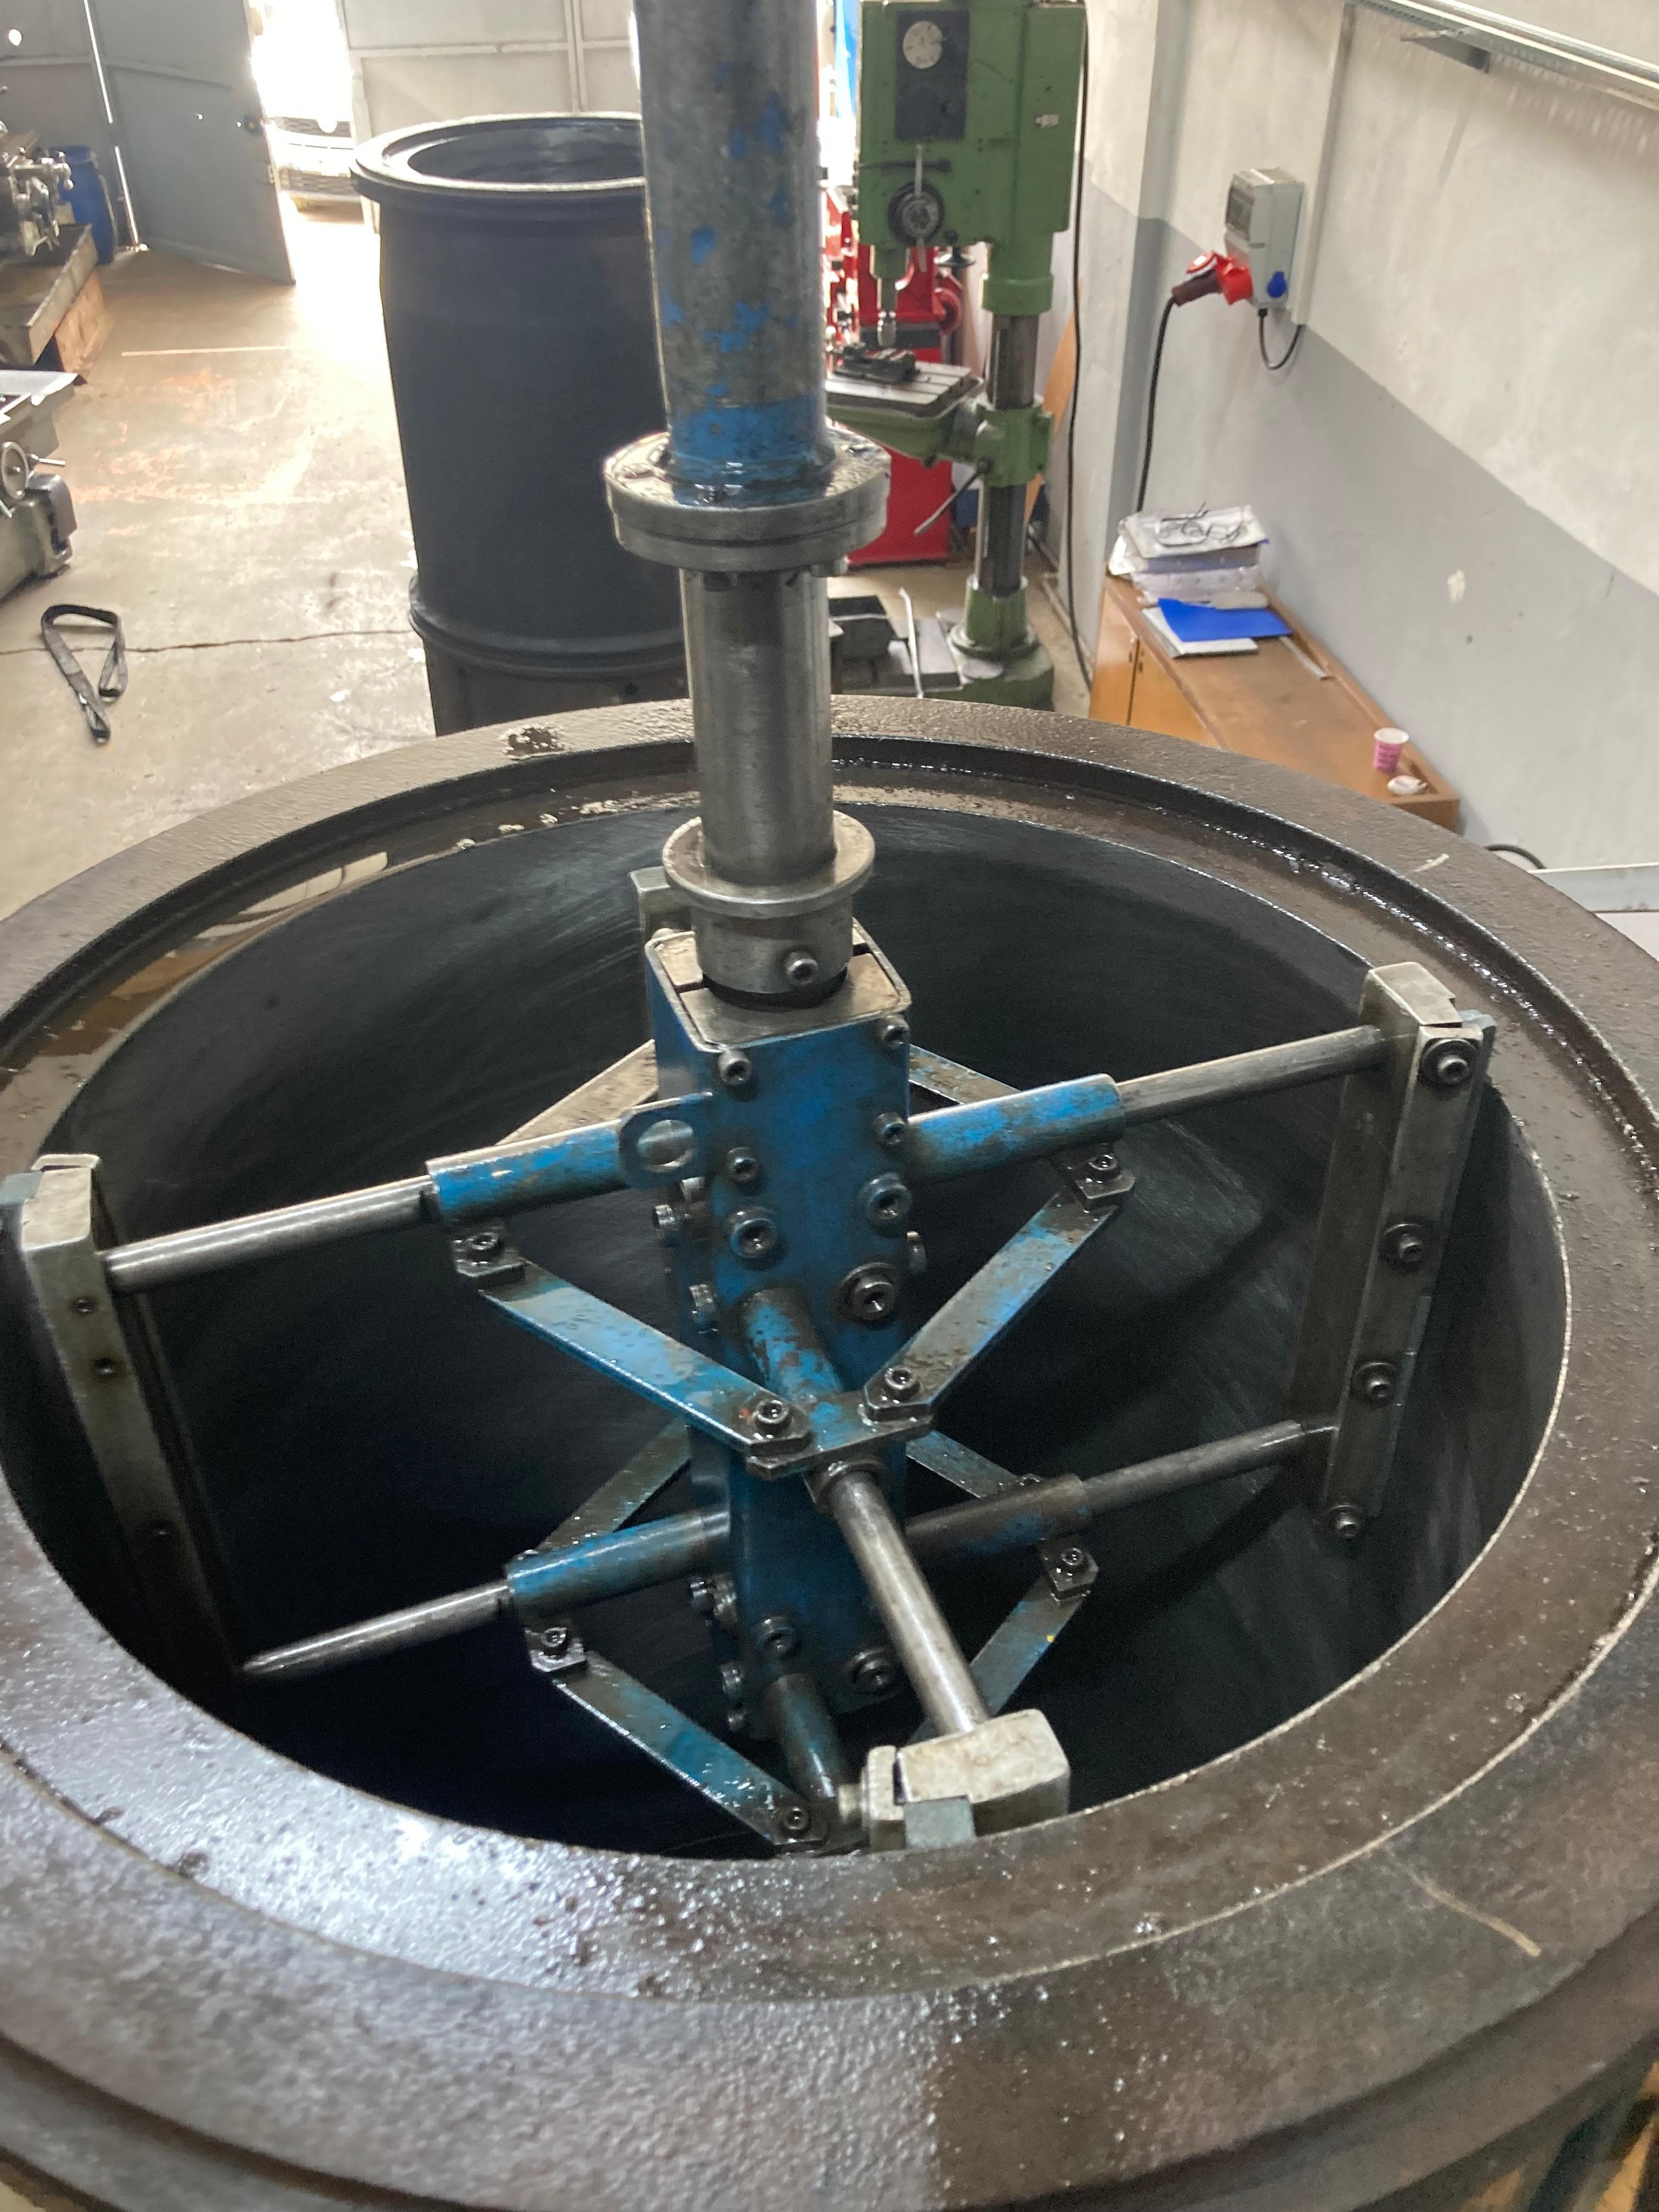
On board, with the liner in place: the glazed layer in the bore is removed with honing stones and the cross-hatch that holds oil for the piston rings is restored. It is not a dimensional correction.
A glazed liner bore does not hold oil; the rings do not bed in properly, and oil consumption and blow-by rise. Honing is done with the machine set up on top of the engine.
Photos from the Job
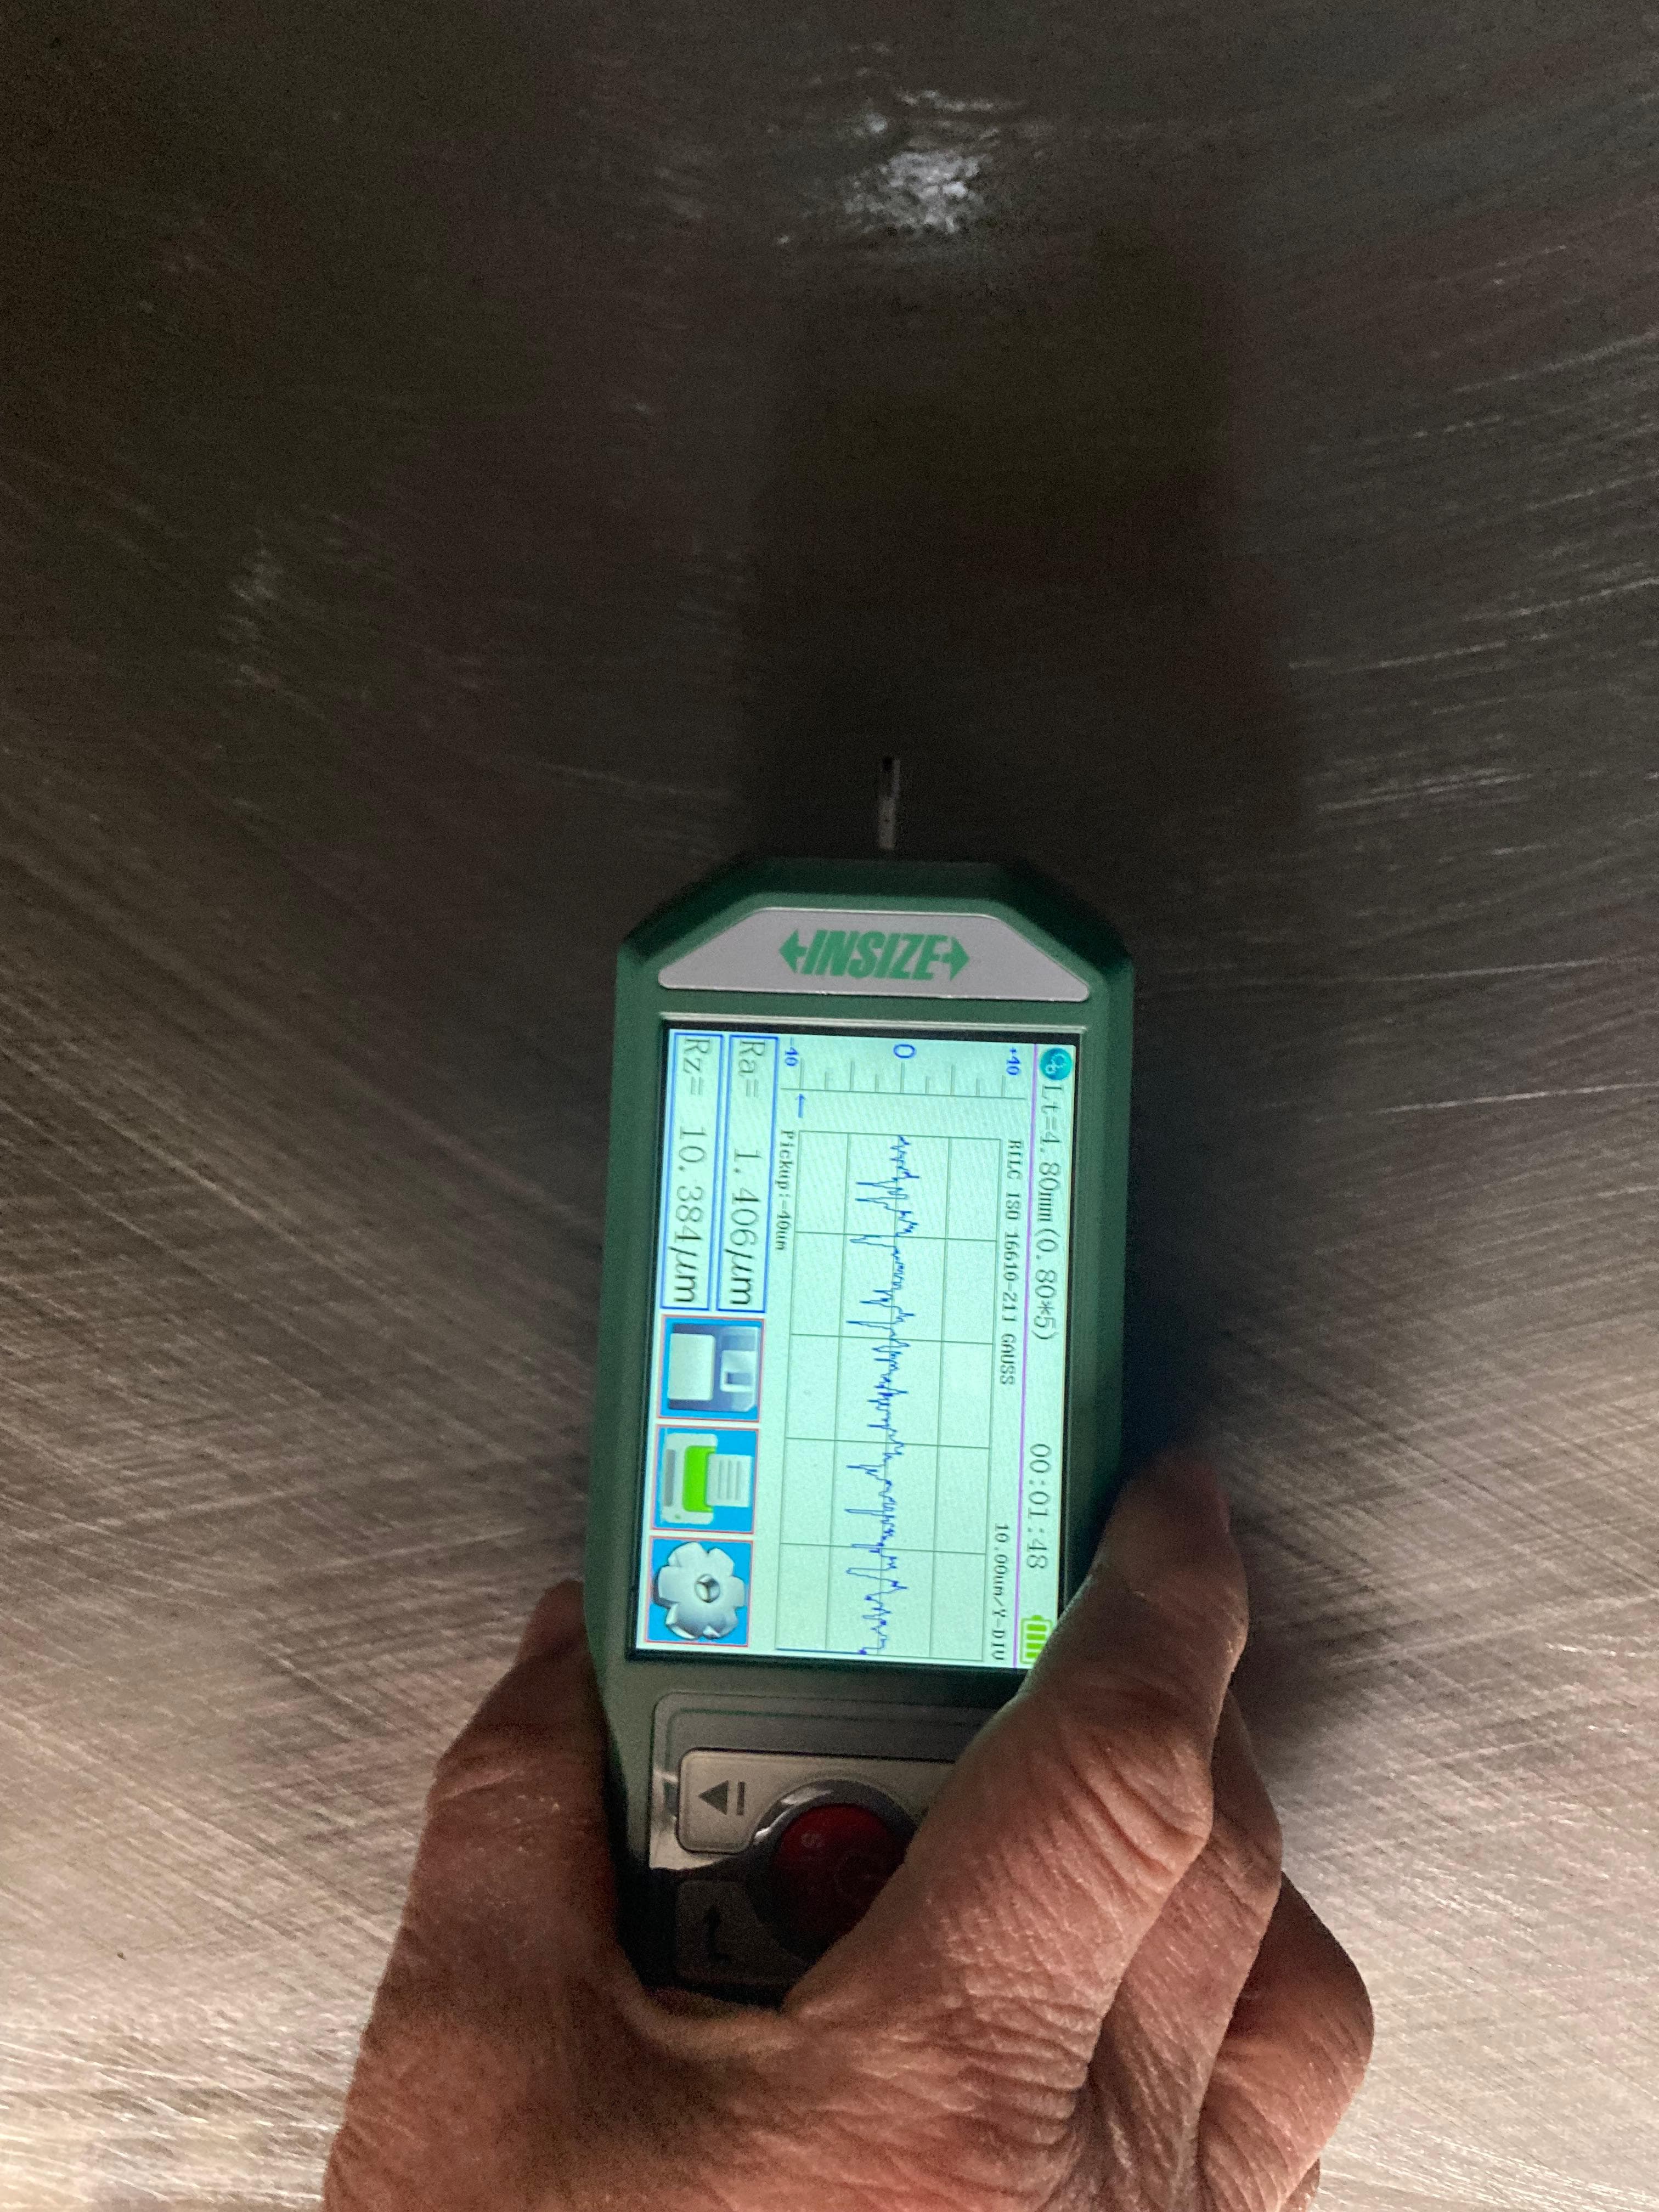
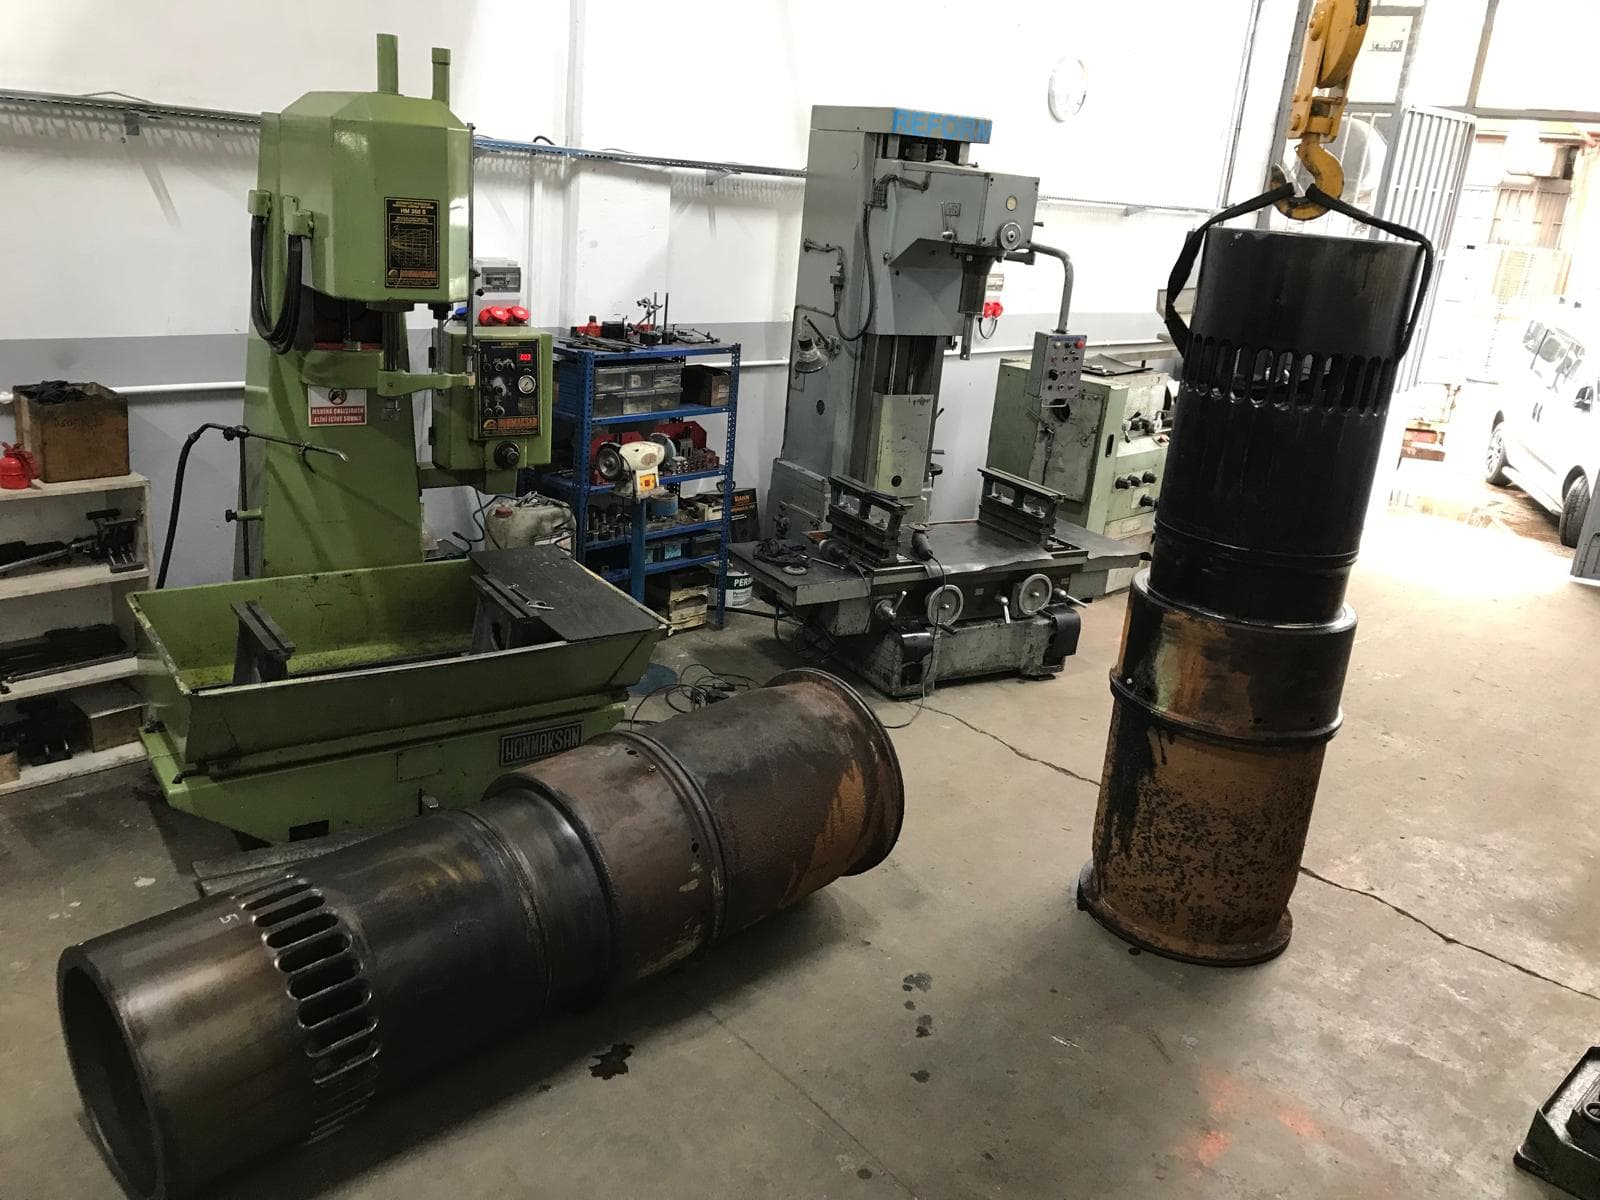
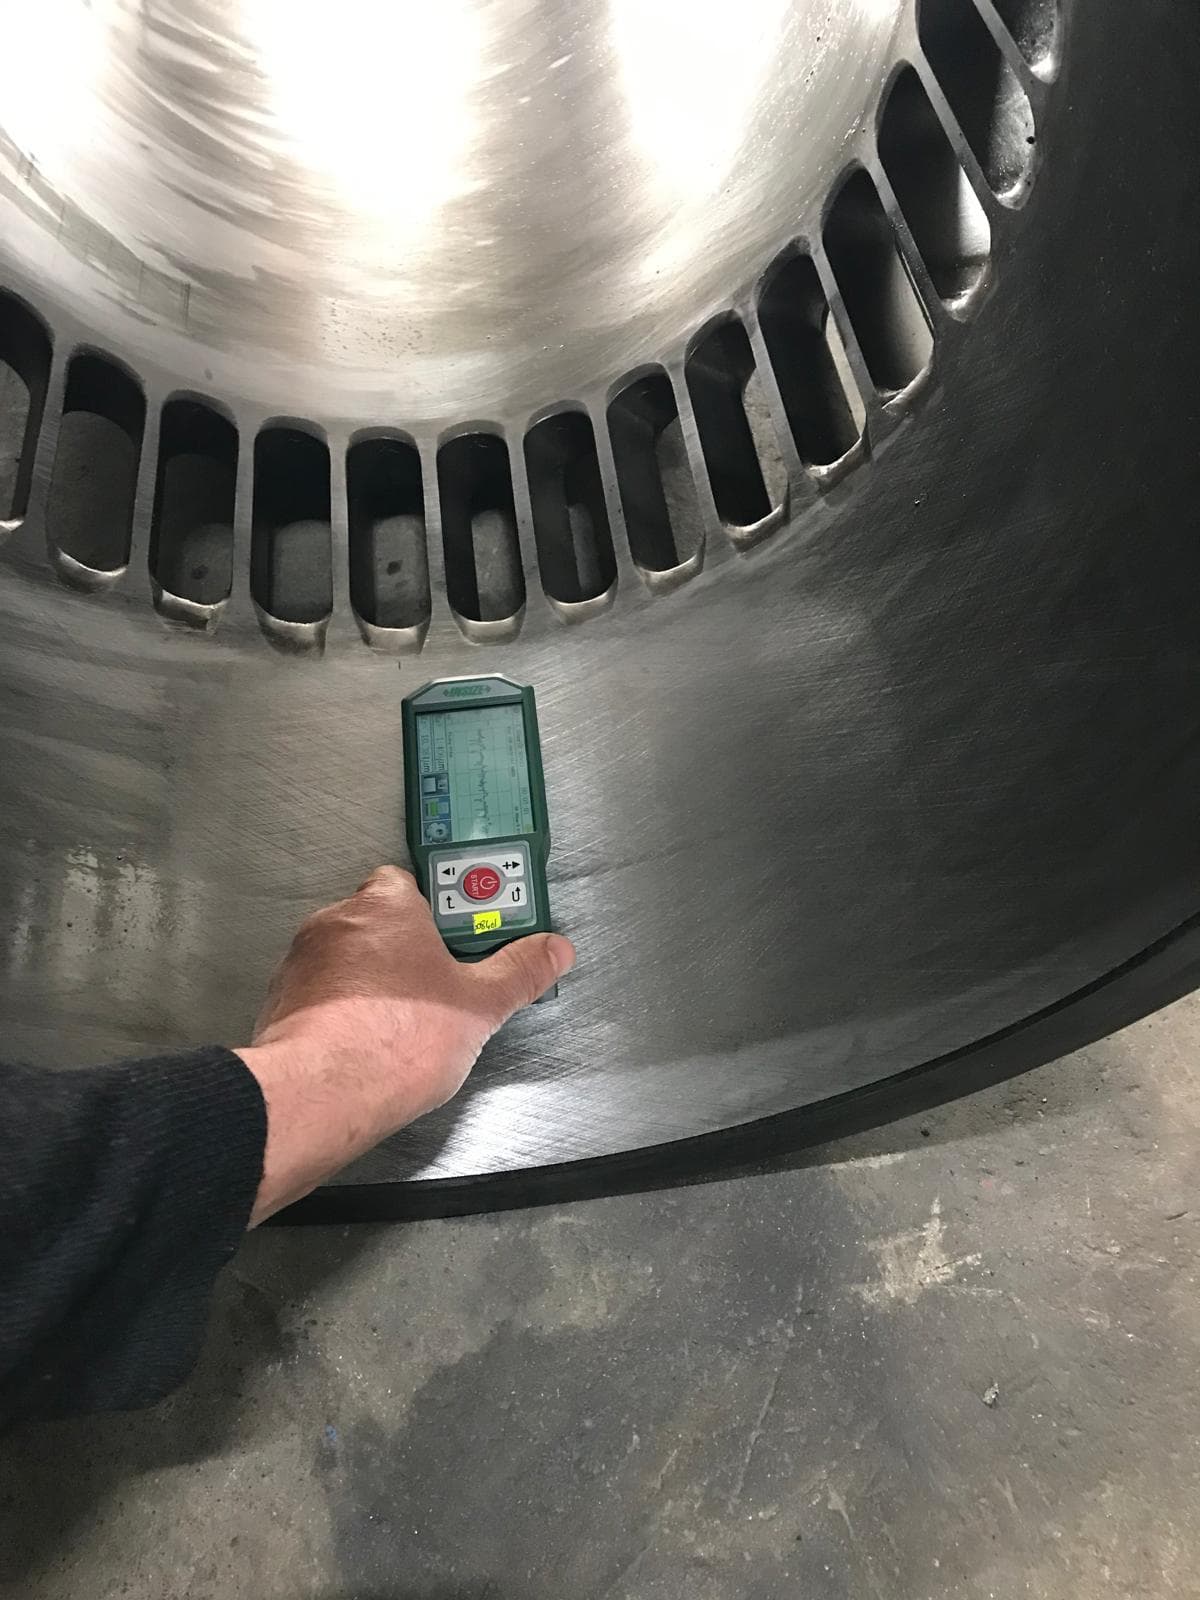
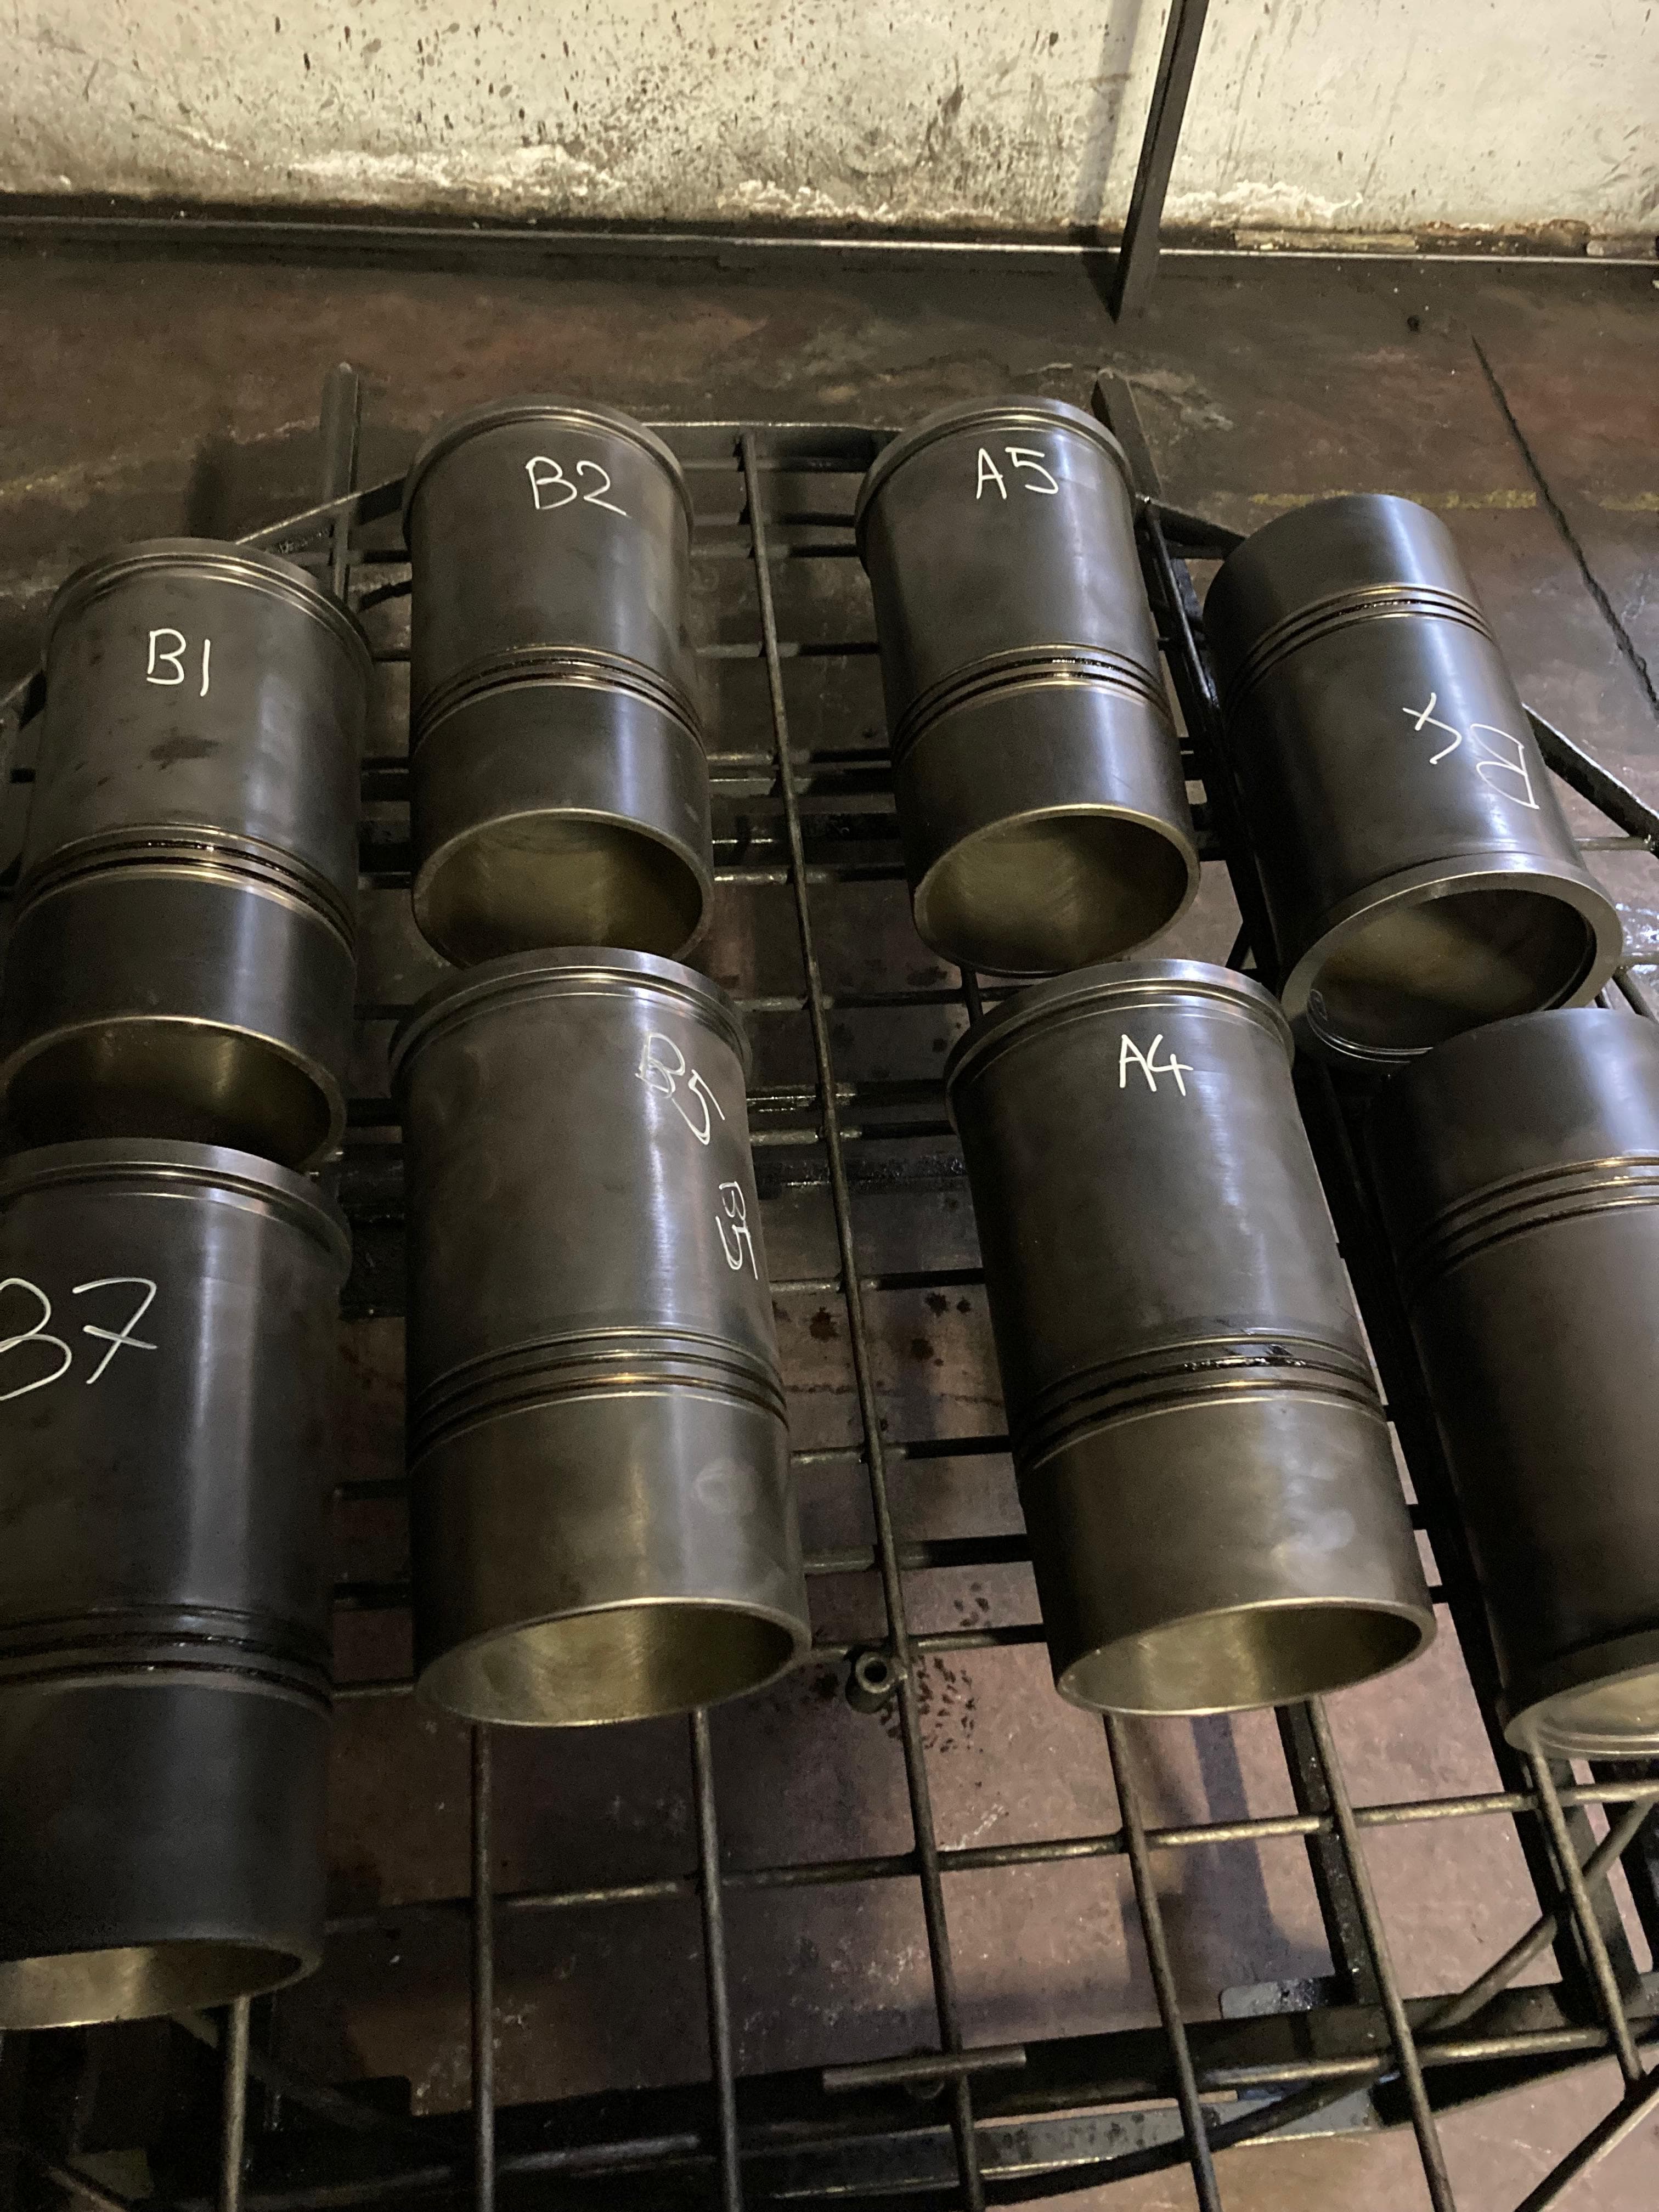
Process Steps
When It Is Needed
- When the bore is mirror-glazed
- When lube oil consumption and blow-by rise
- When new rings are to be fitted and need a suitable surface to bed in
- When the bore shows light scratches
Scope and Limits
- Honing is a surface process; it does not correct ovality, taper or wear, and does not remove deep scoring or cracks.
- A liner out of limits must be replaced.
- We do not supply liners or piston rings.
Frequently Asked Questions
Does honing extend liner life?
On a liner within limits it restores oil retention and ring bedding. It does not bring back the diameter of a worn liner.
Why does cleaning after honing matter?
Honing dust left in the engine accelerates ring and liner wear. That is why all abrasive residue is removed at the end of the job.
What liner bores can you hone?
We hone liner bores from 50 mm to 800 mm.
Can a removed liner be honed?
Yes. A liner taken out of the engine is honed in our workshop.
Contact Us Now
Tell us the engine make and model, the damage and where the vessel is; we will review it and get back to you.
Request a QuoteOther Services
10 servicesOther reconditioning work we do on board and in the workshop.
- In-situ crankpin grinding
- Stress relieving (heat treatment)
- Inspection and reporting
- Crankpin polishing
- Laser alignment check
- Liner seating face grinding
- Crane seating face grinding
- Workshop machining
- Connecting rod crack testing
- Liner flange underside grinding